Before the First Chip Flies: The Hidden Fixtures That Make Japanese Quotes Look Expensive
Ask a purchasing manager in Ohio why they chose a lower quote from a domestic shop over a Japanese one, and you will usually hear about price per unit. What they rarely hear about — because nobody puts it on a line item — is the fixture.
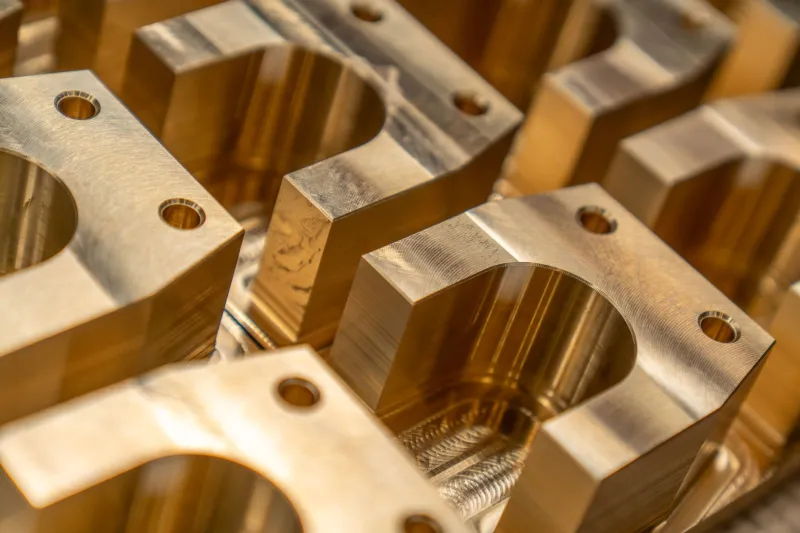
In Japanese precision workshops, the period between accepting a purchase order and cutting the first production part is rarely idle. It is spent designing and building jigs: custom work-holding devices that locate, clamp, and stabilize a workpiece so that the ten-thousandth part comes off the machine identical to the first. For a complex aerospace bracket or a medical housing, that prep can take two to four weeks. The customer sees none of it. The customer only sees a quote that may run ten to fifteen percent higher than a competitor's.
What a Jig Actually Buys You
A jig is not a machine tool. It is often a modest aluminum or steel assembly, sometimes machined in-house, that holds a part in exactly the same orientation for every operation, every shift, every operator. Its purpose is to remove variability from the human element.
The economics are straightforward once you run the numbers. A shop that cuts parts freehand or with generic vises can start shipping tomorrow. But each setup change introduces micro-shifts in datum, and each operator re-learns the part. Over a run of 5,000 units, that shows up as a scatter in critical dimensions — and scatter is what drives inspection cost, rework, and eventually field failures.
A dedicated jig front-loads that cost. You pay once, during tooling prep, and the per-unit defect rate drops accordingly. A workshop running at 99.7% first-pass yield does not get there by inspection. It gets there because the part physically cannot be loaded wrong.
Why the Quote Never Shows It
American buyers are accustomed to seeing tooling charges amortized or itemized on RFQs — a NRE line, a tooling amortization column. Japanese quotes often fold jig-building into the unit price or into a broader preparation fee, and the practice is rarely explained unless asked.
That opacity is a genuine disadvantage in a competitive bid, and it is worth being honest about. A buyer comparing three quotes side by side will not know that the higher Japanese number includes forty hours of fixture engineering. They will only know it is higher.
The corrective is procedural, not motivational. Ask suppliers directly: what work-holding will be built for this part, who owns that tooling at the end of the program, and what happens to the per-unit price at 2,000 units versus 20,000. A shop that has genuinely invested in jigs will answer quickly and in detail. A shop quoting thin will hedge.
The Long-Run Math American Buyers Underweight
There is a cultural dimension here that goes beyond accounting. Japanese manufacturing practice treats the fixture as an asset that outlives the purchase order. Workshops routinely retain and catalog jigs for years, so that a reorder eighteen months later starts production in days, not weeks, with the original datums intact. The jig is a memory of the program.
For a US buyer, that translates into something procurement spreadsheets rarely capture: reorder stability. The second production run behaves like the first. Dimensional data from the initial PPAP still applies. There is no requalification scramble.
Contrast that with the low-quote alternative, where a re-order means re-fixturing from scratch, new setup variation, and a fresh round of first-article inspection. The savings from the cheaper quote get spent the second time around.
How to Shop for the Jig, Not Just the Part
Three practical moves for any buyer evaluating an overseas or domestic supplier:
Ask for the fixturing plan as a deliverable. Not a promise — a document. Sketches, datum strategy, clamping sequence. Shops with real capability produce this without complaint.
Price the second order, not the first. Ask what changes on a reorder. If nothing has been retained, you have learned something important about how that shop thinks about your program.
Ask who owns the tooling. In Japanese practice, the customer typically does, even when the jig never appears on an invoice. Getting that in writing protects you if you ever move the work.
None of this guarantees a Japanese supplier is the right choice for every part. Low-volume, tolerance-forgiving work often genuinely is better done fast and cheap, without bespoke fixtures. But for programs where repeatability across years matters more than the first invoice, the invisible weeks of jig-building are not overhead.
They are the quiet reason the price holds.